Most striping contractors and municipal project managers focus on forward travel speed, engine horsepower, and chassis ergonomics when purchasing equipment. However, road striping crews encounter the most severe downtime when fluid systems fail. Uneven line edges, premature packings failure, pressure drops, and clogged spray tips rarely originate in the chassis.
At HVBAN, we build road striping machinery from the fluid delivery system outward. A striping rig is not just a utility cart; it is an industrial displacement system designed to meter, pressurize, and atomize abrasive fluids under severe duty cycles.
If you evaluate line striping equipment purely as a vehicle, you risk buying an undersized pump that overheats paint, shears binders, or ruins line profiles. This guide breaks down the selection process through fluid mechanics, rheology, and mechanical engineering so you can specify the right machine for your project portfolio.
Planning an upcoming equipment tender or fleet upgrade? Contact our engineering team today to review your coating specs and receive a detailed system configuration.
.webp?t=1790652088732 "paint marking machine")
1. Coating Chemistry and Fluid Compatibility
Every line striper is fundamentally a metering and atomization platform for specialized chemicals. Choosing the wrong pump architecture for your specific road marking paint creates immediate field failures.
Viscosity and Shear Sensitivity
Traffic paints differ significantly from architectural coatings. They contain high concentrations of solids, such as calcium carbonate, titanium dioxide, and quartz extenders, to endure tire impact and weathering.
Standard waterborne and solvent-based paints require working pressures between 1,800 and 3,000 PSI to achieve complete atomization without thinning. Thinning road paint violates regional VOC regulations and compromises dry times. An airless road marking machine equipped with a positive displacement piston pump atomizes these heavy paints cleanly, delivering sharp borders without edge feathering.
Certain paints suffer binder degradation when subjected to high shear rates. If fluid passages are too narrow, the pressure drop generates frictional heat that destabilizes waterborne emulsions. This causes paint to coagulate inside the manifold. Fluid passages must maintain consistent inner diameters to prevent velocity spikes.
Single-Component vs. Two-Component (2K) Cold Plastic
Single-component acrylics remain liquid until the solvent or water evaporates. Dual-component chemistries, such as MMA (methyl methacrylate) or 98:2 cold plastic, rely on an exothermic chemical reaction initiated by a catalyst like benzoyl peroxide (BPO).
When selecting a cold plastic marking machine, you must choose between two distinct fluid processing philosophies:
External Mixing: The base resin and catalyst leave separate spray tips and mix mid-air or directly on the road surface. This approach eliminates the risk of resin setting inside the pump or manifold if a crew member stops spraying unexpectedly. However, ambient wind can alter the mixing ratio and compromise paint curing.
Internal Mixing: Resin and catalyst combine inside an active or static mixing chamber directly before the nozzle. This provides thorough chemical blending, complete curing, and superior film durability. However, it requires a dedicated solvent flush system. If your crew delays a flush sequence by three minutes, the fluid section will seize permanently.
Wear-Resistant Wetted Parts
Road paint is abrasive. As thousands of gallons pass through a pump, suspended solids act like liquid sandpaper on internal surfaces.
Standard carbon steel or unhardened stainless components wear down rapidly under these conditions. Look for a road line striper manufacturer that installs industrial-grade materials on all wetted surfaces:
Tungsten Carbide Valve Seats: Fluid check valves cycle millions of times. Carbide seats resist micro-pitting, which prevents pressure bleed-off when cycling under full load.
Ceramic or Hard-Chrome Plungers: Micro-polished ceramic and industrial hard-chrome rods reduce friction against packings, extending operational life between rebuilds.
Self-Adjusting Packings: Spring-loaded, V-ring fluid packings automatically compensate for natural wear, stopping external throat leaks before they start.
2. Pump Technologies: Piston vs. Diaphragm Systems
The fluid pump dictates pressure consistency, film thickness stability, and line definition. Most commercial machines utilize either diaphragm pumps or hydraulic piston pumps.
Diaphragm Pumps: Low Cost, Severe Viscosity Limits
Diaphragm systems utilize an oscillating flexible membrane to cycle paint. They cost less upfront and have fewer moving mechanical parts exposed directly to the fluid.
However, diaphragm pumps deliver limited mechanical advantage. When fluid viscosity rises on cold mornings, diaphragm intake check valves struggle to seat, starving the fluid section. Furthermore, diaphragm discharge exhibits a noticeable pressure pulse at stroke transition. This pulse produces an uneven, "snakeskin" edge on the road line, making it hard to pass strict municipal line-width inspections.
Hydraulic Piston Pumps: The Heavy-Duty Standard
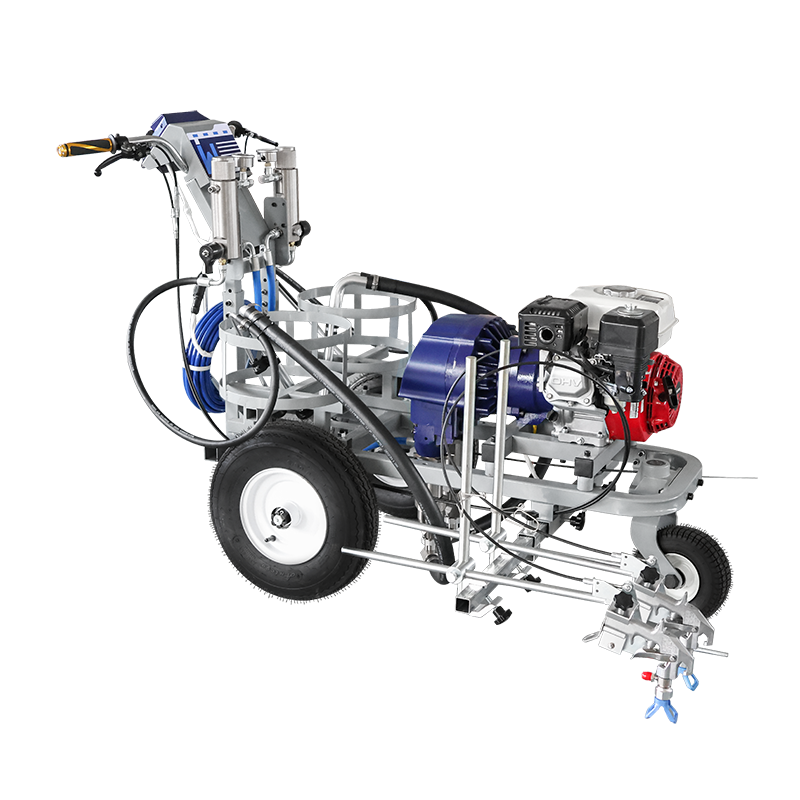
Modern industrial striping operations rely heavily on hydraulic paint marking equipment. In these systems, an engine-driven hydraulic pump powers a hydraulic motor, which cycles a heavy-duty fluid piston through a long, continuous stroke.
A hydraulic piston pump delivers continuous, unyielding torque throughout the entire stroke. This yields significant performance advantages:
Zero Pulse Drop: The electronic or mechanical shift mechanism switches stroke direction in milliseconds, maintaining steady tip pressure and sharp edge definition.
High Viscosity Pumping: Direct-immersion foot valves sit low in the paint container, using gravity and vacuum to draw heavy, unthinned coatings easily.
Slower Cycle Speeds: Large-displacement fluid sections deliver high flow rates at low cycle frequencies. Fewer cycles per minute minimize friction, running cooler and lasting longer than fast-cycling direct-gas mechanical rigs.
Sizing the Pump: Flow Rates and Orifice Sizing
Never size your paint pump for line striper setups based on average speed alone. Size it against your peak fluid demand. Peak fluid demand depends on gun count, line width, mil thickness, and maximum travel speed.
Consult this fluid sizing formula before purchasing:
Required Flow (GPM) = Line Width (inches) × Wet Film Thickness (mils) × Speed (MPH) × 0.007
To run two spray guns simultaneously using .023-inch tips, the system must support a minimum fluid delivery of 1.25 Gallons Per Minute (GPM) without dropping working pressure. Sizing a pump to run at 90% capacity continuously causes premature hydraulic oil breakdown and valve failure. Run your pump at 60% to 70% of continuous flow capacity to maintain operational headroom.
3. Application Matrix: Matching Machinery to Operational Demands
Every commercial application presents unique physical and environmental constraints. Use this matrix to match your site requirements with the right machine platform.
Warehousing, Logistics Centers, and Indoor Facilities
Indoor striping projects prohibit the use of internal combustion engines due to carbon monoxide risks and noise levels. Furthermore, indoor epoxy and polyurethane floor markings require ultra-crisp edges without overspray misting.
Power Source: High-capacity lithium-ion or sealed AGM battery drives.
Fluid System: Closed-loop electric airless road marking machine running fine-finish reversible tips.
Key Feature: Integrated vacuum containment or mechanical overspray shields to keep paint off surrounding inventory.
Municipal Roadways and Urban Intersections
City road striping demands high mobility, frequent stop-and-start cycles, and rapid color changes for white and yellow traffic lines.
Power Source: Commercial gas engines driving an independent hydraulic propulsion system.
Fluid System: Dual-pump paint marking machine setup with completely separate fluid paths to eliminate flush times between colors.
Key Feature: Pressurized glass bead delivery systems linked to line-gun triggers via delay timers for immediate reflective bead embedment.
Airports, Runways, and Highway Infrastructure
Long highway lines and wide runway markings (up to 36 inches across) require massive fluid output and large onboard capacity.
Power Source: Ride-on diesel or gas hydraulic power plants.
Fluid System: High-output hydraulic paint marking equipment supplying multiple guns with paint outputs exceeding 4.0 GPM.
Key Feature: Automated skip-line controllers, self-centering steering systems, and bulk-tote paint intake manifolds.
4. Total Cost of Ownership (TCO) and Downtime Control
A striping crew costs between $150 and $400 per hour in labor, traffic control, and management overhead. If a fluid pump seizes on an active highway closure, you lose money long before factoring in replacement parts. The purchase price of a paint marking machine represents only 20% to 30% of its real lifecycle cost.
Field-Serviceable Modular Fluid Sections
When pump packings fail in the field, your crew faces two options: spend four hours disassembling the unit on the roadside, or swap the fluid section out in minutes.
HVBAN designs equipment around quick-detachable fluid sections. Operators can loosen a retention nut, slide out the worn lower pump unit, drop in a pre-packed replacement, and resume spraying in under ten minutes. The worn pump lower can then be serviced back in the shop under clean conditions.
Hydraulic Oil Cooling Efficiency
Hydraulic pumps generate heat under sustained heavy loads. When hydraulic fluid temperatures exceed 160°F (71°C), the oil thins out, reducing volumetric efficiency and wearing internal seals.
Check the hydraulic reservoir size and heat exchanger layout before buying. Undersized hydraulic reservoirs save frame space but lead to shortened pump life in warm climates. Look for large-capacity fluid reservoirs with integrated external cooling fans.
5. Engineering-Grade Equipment Evaluation Checklist
Review these critical mechanical specifications with prospective manufacturers before signing a purchase contract:
1. Coating Compatibility: Is the fluid packings package compatible with your specific paint chemistry (waterborne, solvent, MMA, 2K epoxy)?
2. Pump Displacement Rate: What is the fluid output per cycle, and what engine RPM is required to maintain maximum line pressure?
3. Fluid Section Accessibility: Can the pump lower be removed without disassembling the engine or hydraulic drive connections?
4. Valve Seat Materials: Are intake and discharge valve seats constructed from solid tungsten carbide or treated tool steel?
5. Hydraulic Cooling System: Does the system feature a dedicated, fan-assisted oil cooler rated for ambient operation above 100°F (38°C)?
6. Glass Bead Delivery Architecture: Is the bead tank an unpressurized gravity box, or an ASME-certified pressure vessel delivering forced bead embedment?
7. Spare Parts Support: Does the equipment supplier maintain regional inventory for common consumables (tips, packings, filters, valves) for immediate dispatch?
Specifying a paint marking machine requires balancing fluid rheology with mechanical output. Choosing the right fluid delivery platform ensures uniform film builds, sharp lines, and uninterrupted field production.
Have technical questions about matching a pump to your paint specs? Submit an inquiry to HVBAN's engineering team. We provide complete fluid-compatibility reviews and custom manufacturing options for global striping projects.
Frequently Asked Questions
Q1: Why does paint leak from the throat packing nut during spraying?
A1: Throat packings naturally compress and wear during operation. If the packing nut loosens, fluid bypasses the upper seals. Minor leakage can often be corrected by tightening the packing nut one-quarter turn and adding Throat Seal Liquid (TSL) to prevent dried paint from tearing the seals. If leakage continues, the V-packings are worn out or the piston rod is scored, requiring a lower fluid section rebuild.
Q2: Can I apply two-component cold plastic materials using a standard airless road marking machine?
A2: No. Standard single-pump airless machines cannot proportion or mix 2K materials safely. If mixed paint cures inside standard fluid lines, the entire pump lower, high-pressure hose, and spray manifold must be thrown away. Two-component chemistries require dedicated, off-ratio fluid metering circuits (such as 98:2 or 1:1 systems) featuring integrated, emergency solvent purge loops.
Q3: How do I eliminate pressure drops when triggering the spray gun?
A3: Pressure drop usually indicates that your spray tip orifice exceeds the pump's continuous flow output, or the paint intake line is partially obstructed. First, confirm the fluid inlet filter and gun mesh filter are completely clean. If the filters are clear, drop down one spray tip size (e.g., from a .023 to a .021) or upgrade to a higher-output hydraulic paint marking equipment platform.
Q4: What is the true functional advantage of a hydraulic piston pump over a mechanical gas-driven pump?
A4: Mechanical gas-driven pumps use gears and eccentric linkages to stroke the piston at high frequencies. This rapid movement causes pressure spikes, seal friction, and tip wear. Hydraulic piston systems use smooth fluid pressure to stroke the piston lower and slower while displacing more volume per stroke. This delivers a completely flat pressure curve, zero line edge pulsing, and longer fluid seal lifespans.
Q5: How does tip wear affect both line quality and material costs?
A5: As abrasive paint passes through a carbide tip orifice, the opening widens and rounds out. A tip rated at .019 inches can wear to .023 inches after a few thousand feet of continuous work. This wear widens the spray pattern, decreases atomization quality, and increases paint output by up to 30%. Replacing worn tips immediately protects line dimensions and prevents costly paint over-application.