Every road marking contractor has witnessed the consequences of poor equipment matching. You purchase an expensive commercial traffic paint, load it into a rig, and face constant tip clogs, uneven film builds, or excessive fogging. A crew might blame the paint formulation or tip wear, but the root cause usually lies in a mismatch between the paint rheology and the pump output.
Selecting a professional striping machine requires looking past basic engine horsepower. The primary specification that governs your line quality, application speed, and material handling is hydraulic fluid flow rate, measured in gallons per minute (GPM) or liters per minute (LPM). Without sufficient volume delivery at sustained operating pressures, consistent line geometry remains impossible.
Whether you operate small push units or heavy-duty dual-gun setups from manufacturers like HVBAN, matching pump capacity to specific paint properties directly impacts your bottom line. This guide examines how fluid dynamics, paint viscosity, and jobsite variables dictate the exact flow volume required for your projects.
.webp?t=1789886303142 "professional striping machine")
Understanding Flow Rate: Why GPM and LPM Dictate Striping Integrity
Flow rate defines fluid displacement over time. In pavement marking, contractors often confuse high operating pressure with high flow rate. A pump may generate 3,000 PSI at static shutoff, yet fail completely when a spray gun opens under continuous load.
When the gun trigger pulls, fluid exits the orifice, causing immediate line pressure decay. A professional striping machine must instantly replace that evacuated volume to maintain continuous atomization. If your pump flow rating is too low, fluid pressure crashes at the spray tip, resulting in uneven paint distribution and jagged line edges.
Pavement striping operates on a strict mechanical triangle: Flow Rate, Tip Orifice Size, and Ground Speed. These three components determine your final Wet Film Thickness (WFT), calculated in mils or microns.
Flow Rate (GPM/LPM): The maximum volume of paint the fluid section can deliver without cavitation.
Tip Orifice: The aperture restriction that translates hydraulic volume into an atomized fan pattern.
Ground Speed: The rate of forward motion (MPH or km/h) that distributes that spray pattern across the surface.
If you increase forward speed to finish a highway project faster, you must increase the fluid volume output proportionally. If your striping machine cannot deliver the required GPM, your wet film thickness drops below municipal project specifications, triggering inspection failures and expensive rework.
Pavement Paint Rheology vs. Machine Flow Requirements
Road marking materials differ drastically from architectural coatings. Pavement formulations contain high mineral loading, heavy pigments, and specific polymer emulsions engineered for rapid drying and abrasion resistance. Their rheology—how they deform and flow under shear stress—dictates pump requirements.
Most industrial traffic paints are shear-thinning (thixotropic). They appear thick in the drum but thin out when forced through small fluid passages under pressure. If a pump cannot supply continuous volume, shear rates fluctuate, causing the paint to re-thicken prematurely inside the manifold or spray gun.
| Pavement Paint Type | Viscosity Range (Krebs Units - KU) | Solids by Volume | Recommended Minimum Flow Rate |
|---|---|---|---|
| Standard Waterborne Acrylic | 75 - 90 KU | 55% - 62% | 0.50 - 1.25 GPM (1.9 - 4.7 LPM) |
| High-Solids Fast-Dry Acrylic | 85 - 110 KU | 65% - 78% | 1.25 - 2.50 GPM (4.7 - 9.5 LPM) |
| Solvent-Based Chlorinated Rubber / Alkyd | 70 - 85 KU | 50% - 60% | 0.60 - 1.25 GPM (2.3 - 4.7 LPM) |
| Plural Component MMA (Cold Plastic) | 100+ KU (Thixotropic Paste) | 95% - 100% | 2.00 - 4.00+ GPM (7.5 - 15.1 LPM) |
Standard Waterborne Traffic Paints
Modern waterborne paints dry through water evaporation and particle coalescence. They typically carry a viscosity rating between 75 and 90 KU. These paints move smoothly through standard fluid sections, requiring moderate flow rates between 0.50 and 1.25 GPM for standard 4-inch lines at walking speeds.
High-Solids and Low-VOC Formulations
State and national environmental mandates have pushed road agencies toward high-solids waterborne formulations. These paints reduce VOC emissions but introduce heavy aggregate loads and thick binders. They demand rapid displacement and constant displacement force. A professional striping machine handling high-solids paint requires a minimum output of 1.25 to 2.50 GPM to prevent system pressure drops and severe tip plugging.
Two-Component / MMA Materials
Methyl methacrylate (MMA) and cold plastic materials represent the most demanding segment of pavement marking. These 98:2 or 1:1 reaction systems exhibit extreme viscosities before blending. Pumping these materials requires heavy displacement piston fluid sections driven by high-output hydraulic systems capable of delivering sustained, high-volume flow under intense head pressure.
Application Scenarios: Sizing the Pump to the Jobsite
Every striping contractor operates across distinct environments. Sizing your equipment based on maximum expected daily workload ensures long mechanical service life while avoiding premature fluid section burnout.
Scenario 1: Commercial Parking Lots and Warehouses
Commercial parking lots involve tight turning radiuses, frequent start-stop sequences, and narrow stalls. Forward application speeds rarely exceed 2 to 3 miles per hour. Contractors lay down single 4-inch lines using quick-drying solvent or standard waterborne paints.
For this application, a professional striping machine delivering 0.50 to 0.75 GPM is ideal. Lower-displacement pumps prevent excessive pressure surges when releasing the gun trigger. They also reduce equipment weight, allowing operators to maneuver cleanly around tight curbs, light poles, and pedestrian islands.
Scenario 2: Municipal Streets and Urban Intersections
City road maintenance crews routinely paint parallel double-yellow centerlines, solid white edge lines, and large crosswalk bars. This environment demands simultaneous dual-gun operation.
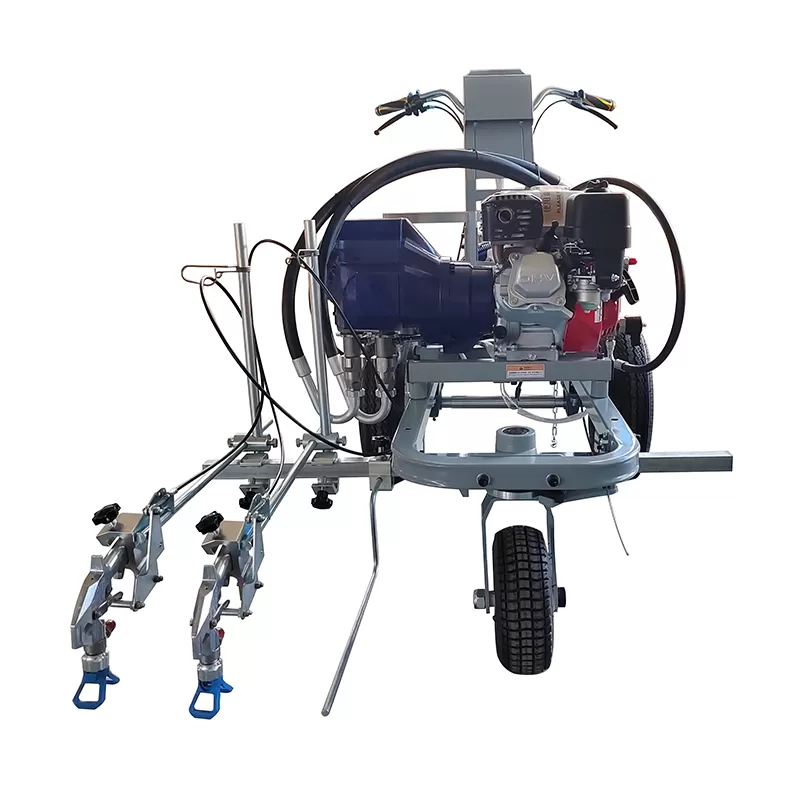
Running two spray guns splits your fluid output. If a machine produces 1.0 GPM, each gun receives a maximum of 0.50 GPM. If you apply high-solids paint through two 0.021-inch tips, the system can starve, causing pressure drops and line tapering. Municipal operations require units rated at 1.25 to 2.0 GPM. Equipment like HVBAN hydraulic series stripers provides the fluid capacity necessary to sustain balanced dual-gun pressure across varied road profiles without stalling.
Scenario 3: Highways and Airport Runways
High-production roadway striping focuses on high ground speeds (5 to 10+ MPH) and broad line patterns. Airport runways frequently specify 12-inch, 24-inch, or 36-inch wide solid markings applied in single passes, with wet film requirements reaching 20 to 30 mils.
Achieving this coating depth at speed requires high-volume displacement. Runway and highway contractors operate heavy-duty ride-on platforms delivering 2.50 to 4.0+ GPM. High-output fluid delivery ensures the paint film remains wet long enough for dropped glass beads to sink to their optimal 60% embedment depth, ensuring retroreflectivity compliance.
The Cost of Flow Mismatch: Diagnosing Jobsite Failures
When pump capacity fails to align with material physics, mechanical problems emerge on the pavement. Understanding these failure modes helps field supervisors correct pump issues quickly.
Under-Pumping Failures
Using an undersized pump for high-viscosity coatings creates several immediate issues:
Fingering and Tails: The spray pattern develops heavy, thick outer edges with a hollow center because pressure drops too low to atomize paint across the full fan width.
Line Pulsation: As the piston cycles back and forth, output dips momentarily, resulting in visible washboard patterns on the asphalt.
Accelerated Packings Wear: An undersized fluid section forced to cycle at maximum cycle speeds generates severe friction heat, degrading throat packings and scoring chrome piston rods.
Over-Pumping Failures
While excess pump capacity is generally safer than under-sizing, improperly regulated high-volume delivery also creates specific application challenges:
Severe Paint Fogging: Forcing fluid through small orifices with excessive hydraulic displacement produces fine airborne mist that drifts onto parked cars or adjacent lanes.
Bead Immersion: Applying excessive paint volume leads to overly thick wet films. Reflective glass beads sink completely below the paint surface rather than embedding halfway, eliminating night-time retroreflectivity.
Edge Feathering: Over-pressurized fans create turbulent air currents at the pavement surface, generating ragged, fuzzy borders rather than crisp edges.
System Maintenance: Protecting Flow Integrity Over Time
A professional striping machine may leave the factory rated for 2.0 GPM, but field conditions rapidly degrade that volume if crews neglect basic maintenance protocols. Flow rate directly relies on the mechanical seal formed inside the displacement pump.
Check valves govern fluid direction. Every pump uses an intake ball valve (foot valve) and an outlet ball valve on the piston rod. Highly abrasive pavement paints, loaded with silica and titanium dioxide, scour these steel components. As the valve balls and carbide seats wear, paint slips past during the stroke cycle, causing internal bypass.
Operators might notice the engine running at normal RPM while the spray tip continuously loses atomization pressure. Inspect and clean fluid check valves weekly. Replace worn balls and seats at the first sign of surface pitting.
Fluid filtration also directly dictates steady flow. Match your manifold and gun filter mesh sizes directly to your paint viscosity and tip selection:
30 Mesh (Green): High-solids paints, heavy elastomeric, and structural coatings.
50 - 60 Mesh (Blue/White): Standard waterborne and solvent traffic paints.
100 Mesh (Yellow): Thin architectural paints, concrete stains, or clear coat sealers.
Using a 100-mesh filter on thick waterborne traffic paint restricts material flow into the delivery hose, creating artificial pressure drops that look like a failing pump.
Frequently Asked Questions (FAQ)
Q1: What is the minimum flow rate required to run two guns simultaneously?
A1: To run dual guns efficiently with standard 4-inch traffic lines, use a machine with at least 1.25 GPM (4.7 LPM). If you spray heavy high-solids waterborne paint through larger tips (such as 0.021-inch or 0.023-inch), aim for a minimum rating of 1.60 to 2.0 GPM to prevent atomization loss during concurrent spraying.
Q2: How does line width affect my machine flow rate selection?
A2: Wider lines require proportionally higher fluid volume. Spraying a single 12-inch line at 15 mils wet film thickness requires three times the fluid output of a standard 4-inch line applied at the same forward speed. Wide lines demand large tip orifices (such as 0.027-inch to 0.035-inch) that rapidly exhaust low-capacity pumps.
Q3: Can I thin high-solids road paint to make it work in an undersized pump?
A3: Do not thin pavement paints beyond manufacturer recommendations (rarely more than 5% by volume). Over-thinning breaks down chemical drying chemistry, extends cure times, causes paint run-off on sloped asphalt, and violates state VOC regulations. Thinning also causes reflective glass beads to sink to the road surface, ruining retroreflectivity.
Q4: Why does my striping machine lose spraying pressure when I increase application speed?
A4: When you increase ground speed while trying to maintain line thickness, you must install a larger tip orifice. The larger tip allows paint to escape the fluid section faster. If your pump displacement rating (GPM) cannot keep pace with this fluid exit volume, line pressure falls and atomization breaks down.
Q5: What is the difference between hydraulic and direct-drive gas striper pumps?
A5: Direct-drive mechanical pumps rely on a mechanical gearbox directly connected to the engine, which produces shorter, faster stroke cycles that can cause pressure pulsation. Hydraulic pumps use hydraulic fluid to push a slow-stroking piston. This design delivers higher continuous flow rates, handles heavier aggregate-loaded paints, and maintains more uniform operating pressure.
Conclusion: Choosing the Right Machine for Reliable Field Output
A professional striping machine must handle the difficult physical realities of your specific coating selections. Choosing equipment solely based on engine size or upfront price often leads to costly project delays, premature pump failures, and lines that fail thickness inspections.
Calculate your daily project scope, understand the shear characteristics of your specified paints, and choose a flow rate that provides at least 20% to 30% mechanical headroom above your base requirements. Commercial manufacturers like HVBAN engineer heavy-duty hydraulic and direct-displacement line marking systems designed to maintain accurate pressures across demanding commercial, municipal, and airport pavement environments.
Do not let equipment mismatches cut into your operational margins. Contact our application engineering team today to review your paint specifications, calculate your required GPM delivery, and request an equipment quote matched directly to your contract needs.